M14 Tap Drill Size (M14 x 2.0)
ISO metric coarse · 2 mm pitch · ISO 261 / 965-1, class 6H
What size drill bit for an M14 tap?
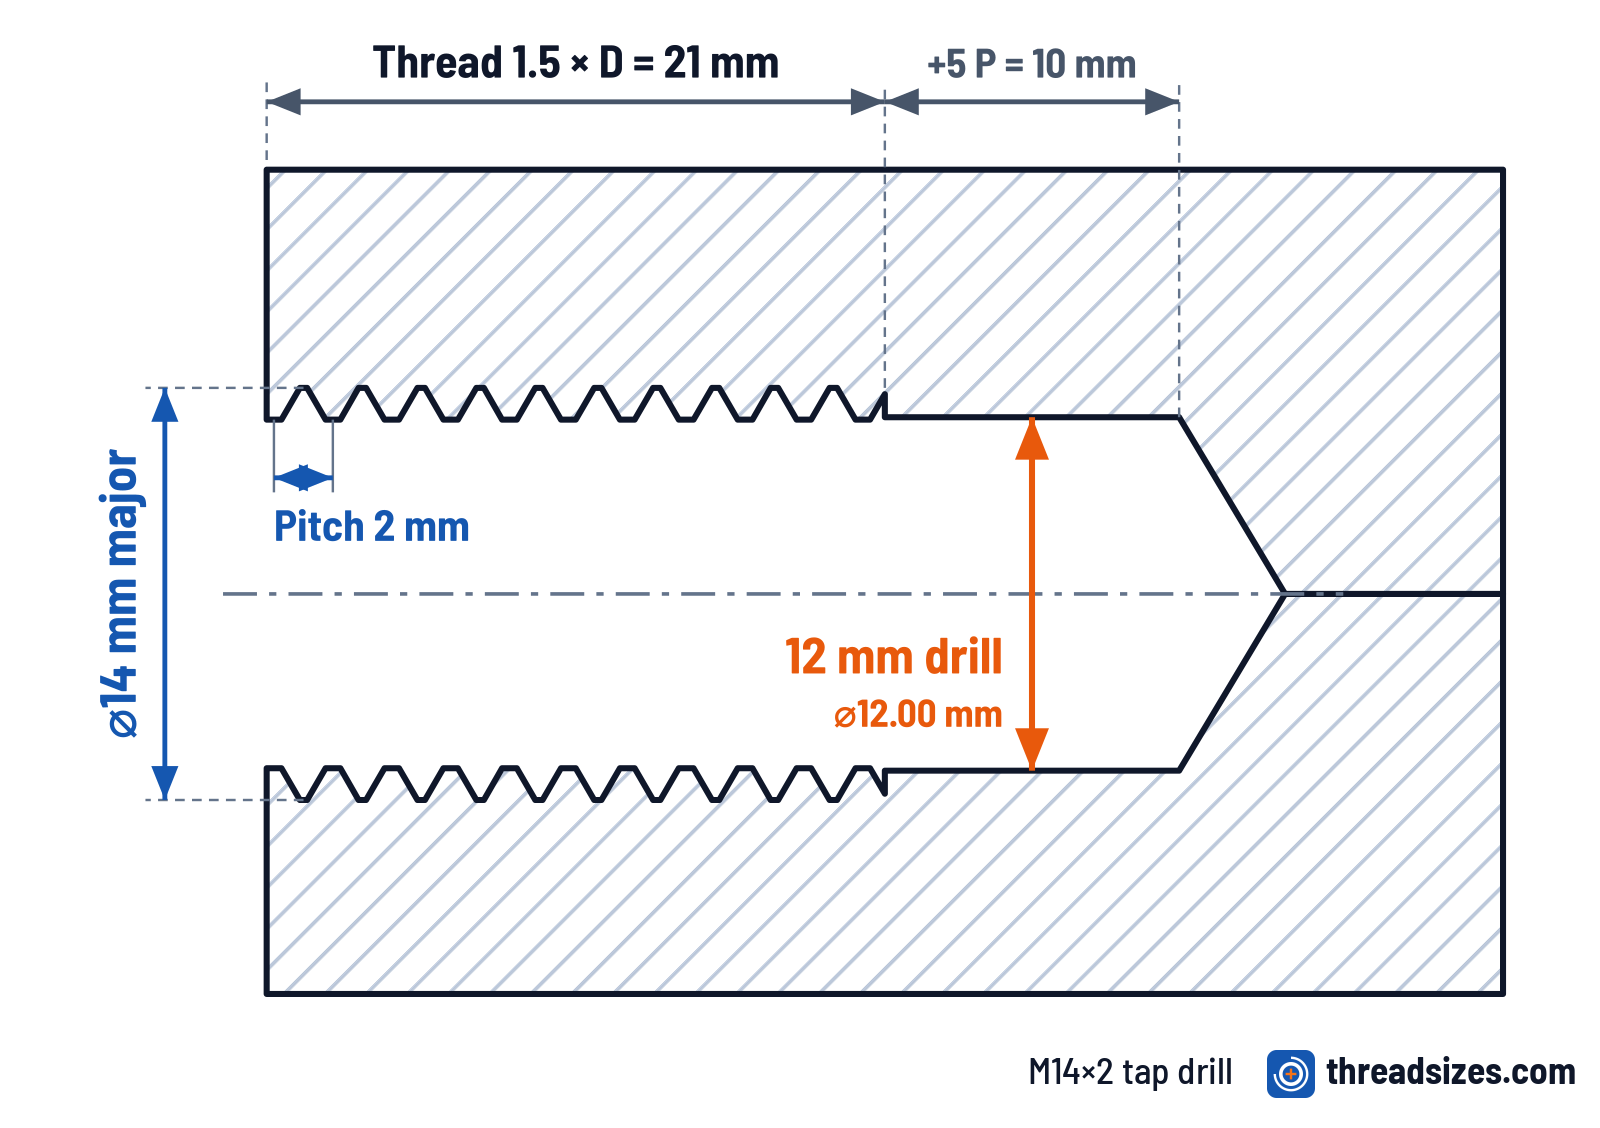
To scale section of the tapped hole
Drawing callout same hole, as a plan note
M14x2-6H ↧21 / ⌀12 ↧31
Thread depth 1.5 × D, drilled 5 pitches deeper for a plug tap; change both to suit your part. Through hole for a screw instead? Use the clearance hole: ⌀15.5 normal fit (ISO 273, clearance hole chart). How to read this →
Drill options % of thread
| Drill | Inch | mm | Thread | 6H |
|---|---|---|---|---|
| 11.8 mm | 0.4646 | 11.80 | ✗ | |
| 11.9 mm | 0.4685 | 11.90 | ✓ | |
| 15/32" | 0.4688 | 11.91 | ✓ | |
| 12 mmUse | 0.4724 | 12.00 | ✓ | |
| 12.1 mm | 0.4764 | 12.10 | ✓ | |
| 12.2 mm | 0.4803 | 12.20 | ✓ | |
| 12.3 mm | 0.4843 | 12.30 | ✗ | |
| 31/64" | 0.4844 | 12.30 | ✗ | |
| 12.4 mm | 0.4882 | 12.40 | ✗ |
By material Aluminum, brass, mild steel: 12 mm (77%) · Stainless, tool steel: 12.2 mm (69%)
75% (orange tick) is the usual target. Hard or gummy metals like stainless are often tapped at 60 to 65% to spare the tap; aluminum, brass and plastic take 75% or a little more. The last column checks the hole against the 6H minor diameter limits (11.83 mm to 12.21 mm).
M14 x 2 ISO 261, 965-1, class 6H
| Major diameter | 14 mm / 0.5512 in |
|---|---|
| Pitch | 2 mm |
| Pitch diameter 6H | 12.701–12.913 mm |
| Minor diameter 6H | 11.835–12.210 mm |
| Thread depth (basic, 5/8 H) | 1.083 mm |
| Forming tap drill (estimate) | 55% 13.5 mm 13.25 mm65% 13 mm 13.12 mm75% 13 mm 12.98 mm |
Forming tap drills are estimates from the rule tap makers use (D − 0.0068 × % × pitch, in inches), shown at 55, 65 and 75% thread with the nearest drill; 65% is the usual starting point. Confirm with your tap maker's chart. Forming taps push the metal instead of cutting it, so never use this drill with a cutting tap.
Clearance hole ISO 273
For a screw that passes through the part. Normal fit is the default; close fit locates the part more accurately but allows less error in hole position. All sizes: clearance hole chart.
Wrench and key ISO 4017, 4032, 4762
Wrench across the flats of a standard hex bolt head and hex nut, and the Allen key for a socket head cap screw. Older DIN 933 heads, still sold, take 22 mm. All sizes in the bolt size chart.
Cross-checks published tables that agree
| Tap drill 12 mm | 2 of 3 |
|---|---|
| Minor diameter 6H | 2 of 2 |
| Pitch diameter 6H | 2 of 2 |
| Clearance holes | 5 of 5 |
| Hex head 21 mm | 3 of 3 |
Tables that list the same value, out of those that list one; a reprint of another table counts once. The other table lists 12.2 mm for the tap drill. How values are checked.
Hole depth rule of thumb
- 14 mmthread engagement to start from in steel (1 × D); the right figure depends on the materials, the thread class and the load
- 21 mmin cast iron or brass (1.5 × D), up to 28 mm in aluminum
- +10 mmextra drill depth below the thread for a plug tap (5 pitches), +4 mm with a bottoming tap
Full table and the ASME B1.1 formula: thread engagement chart.
Shop notes
M14 x 2 is the coarse M14 and the drill is 12 mm, the ISO rule of diameter minus pitch: 14 − 2 = 12. That gives about 77% thread, inside the 6H limits. A 12.1 mm (73%) is a little easier on the tap in stainless.
The inch drill that works is 15/32 (0.4688 in, about 81%, inside the limits). 31/64 looks closer to 12 mm on paper but cuts only about 65% and is over the maximum minor diameter.
M14 sits next to 9/16-12 (14.29 mm, 2.12 mm pitch), and the two get mixed up. M14 x 2 is also common in one spot you might not expect: many spark plugs use a 14 mm thread, but that is the fine M14 x 1.25, not this one.
Tapped M14 x 2?