9/16-18 Tap Drill Size
Unified fine (UNF) · 18 threads per inch · ASME B1.1, class 2B
What size drill bit for a 9/16-18 tap?
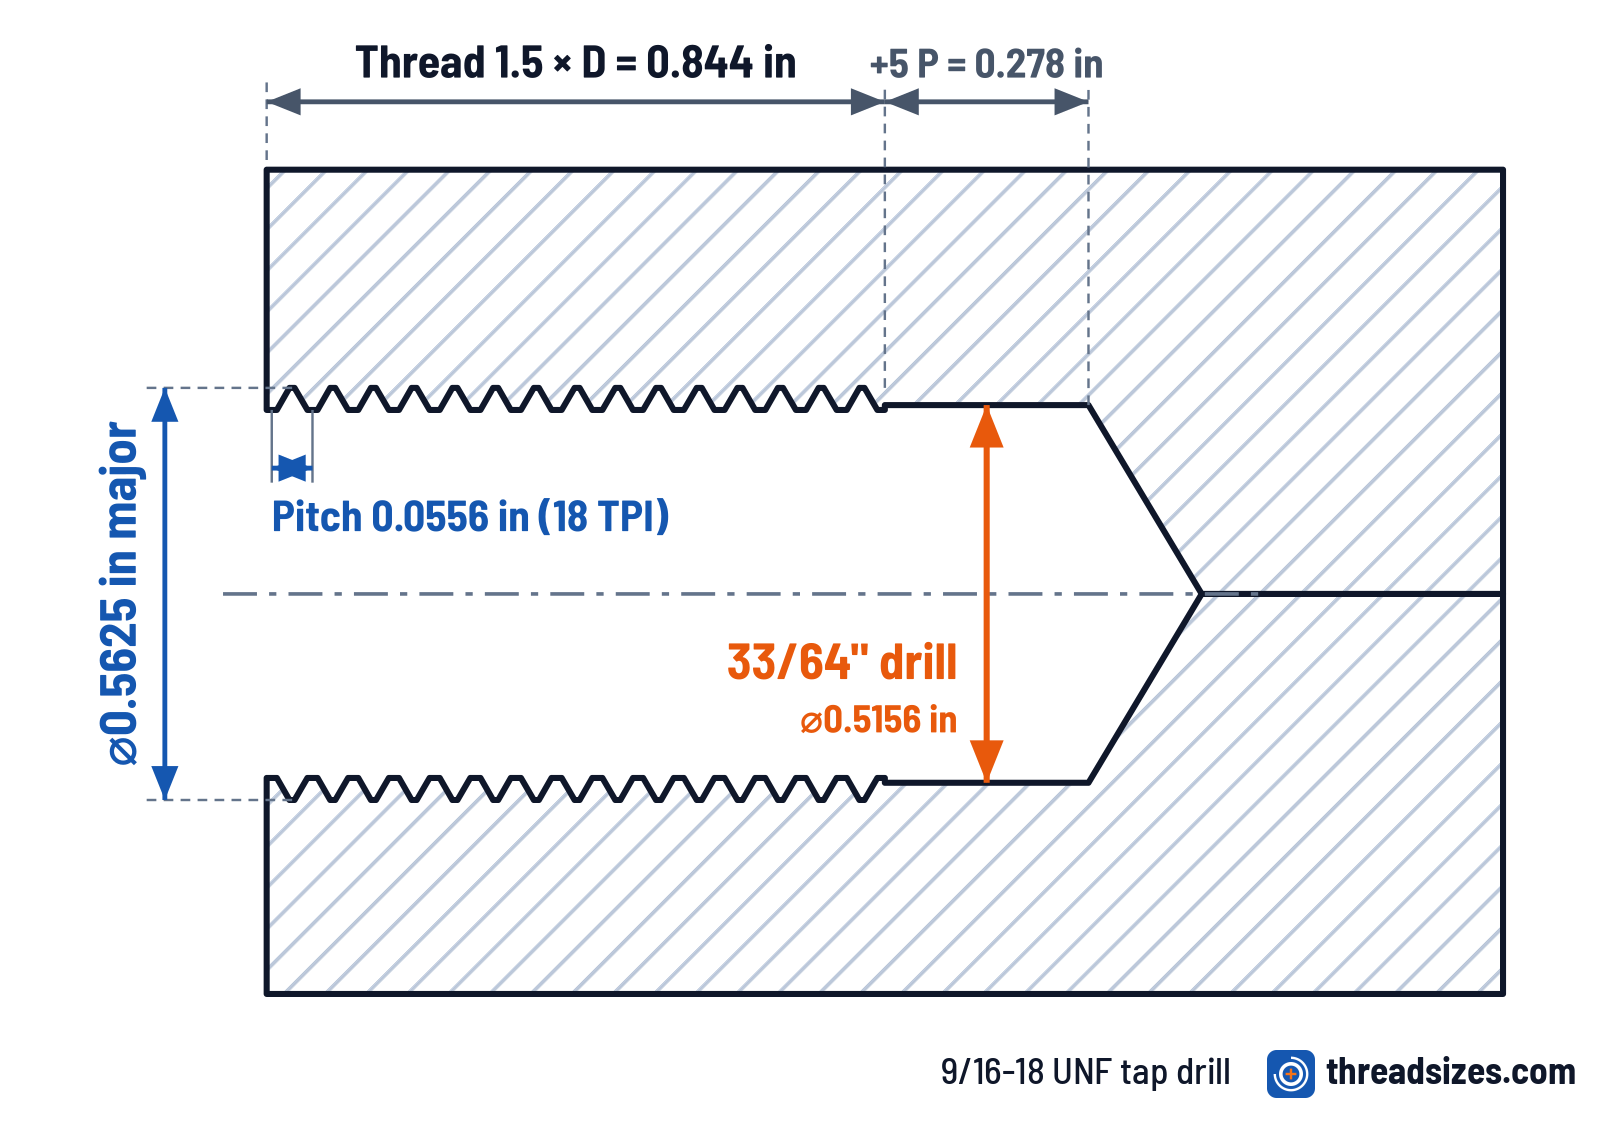
To scale section of the tapped hole
Drawing callout same hole, as a plan note
⌀.516 ↧1.12 / 9/16-18 UNF-2B ↧.84
Thread depth 1.5 × D, drilled 5 pitches deeper for a plug tap; change both to suit your part. Through hole for a screw instead? Use the clearance hole: ⌀.594 free fit (older ASME two-fit chart, clearance hole chart). How to read this →
Drill options % of thread
| Drill | Inch | mm | Thread | 2B |
|---|---|---|---|---|
| 1/2" | 0.5000 | 12.70 | ✗ | |
| 12.8 mm | 0.5039 | 12.80 | ✓ | |
| 12.9 mm | 0.5079 | 12.90 | ✓ | |
| 13 mm | 0.5118 | 13.00 | ✓ | |
| 33/64"Use | 0.5156 | 13.10 | ✗ |
75% (orange tick) is the usual target. Hard or gummy metals like stainless are often tapped at 60 to 65% to spare the tap; aluminum, brass and plastic take 75% or a little more. The last column checks the hole against the 2B minor diameter limits (0.502 in to 0.515 in).
9/16-18 UNF ASME B1.1, class 2B
| Major diameter | 0.5625 in / 14.29 mm |
|---|---|
| Threads per inch | 18 TPI (pitch 0.0556 in) |
| Pitch diameter 2B | 0.5264–0.5323 in |
| Minor diameter 2B | 0.5024–0.5150 in |
| Thread depth (basic, 5/8 H) | 0.0301 in |
| Forming tap drill (estimate) | 55% 35/64" 0.5417 in65% 17/32" 0.5379 in75% 17/32" 0.5342 in |
Forming tap drills are estimates from the rule tap makers use (D − 0.0068 × % × pitch, in inches), shown at 55, 65 and 75% thread with the nearest drill; 65% is the usual starting point. Confirm with your tap maker's chart. Forming taps push the metal instead of cutting it, so never use this drill with a cutting tap.
Clearance hole older ASME two-fit chart
ASME B18.2.8-1999 Table 1 lists only preferred sizes and omits 9/16-18, so this size has no close / normal / loose fit in the current standard. The two drills above are from the older ASME two-fit convention, still reproduced in published charts; the Free value is what shops typically use when a modern “normal” fit is wanted. All sizes: clearance hole chart.
Wrench and key ASME B18.2.1, B18.2.2, B18.3
Wrench across the flats of a standard hex bolt head and hex nut, and the Allen key for a socket head cap screw. All sizes in the bolt size chart.
Cross-checks published tables that agree
| Tap drill 33/64" | 7 of 7 |
|---|---|
| Minor diameter 2B | 2 of 2 |
| Pitch diameter 2B | 2 of 3 |
| Hex nut 7/8 in | 2 of 2 |
Tables that list the same value, out of those that list one; a reprint of another table counts once. How values are checked.
Hole depth rule of thumb
- 0.563 inthread engagement to start from in steel (1 × D); the right figure depends on the materials, the thread class and the load
- 0.844 inin cast iron or brass (1.5 × D), up to 1.125 in in aluminum
- +0.278 inextra drill depth below the thread for a plug tap (5 pitches), +0.111 in with a bottoming tap
Full table and the ASME B1.1 formula: thread engagement chart.
Shop notes
The drill on most charts for 9/16-18 is 33/64 (0.5156 in), and it is a thin choice: about 65% thread, and just over the largest minor diameter class 2B allows. Charts list it because it is the nearest fraction, not because it is ideal.
If you have metric drills, 12.9 mm is the better hole: about 76% thread and inside the 2B limits. A 13 mm (70%) is also inside and easier on the tap in tough steel. Avoid going down to 1/2 in or 12.7 mm: at about 87% they are under the minimum minor diameter.
9/16-18 or M14 x 1.5?
A 9/16 bolt is 14.29 mm across, close enough to M14 x 1.5 (14 mm) to share a drawer, and the pitches are close too: 18 threads per inch is 1.41 mm against 1.5 mm. They still will not swap; the wrong one binds after a few turns. The coarse version, 9/16-12, takes a 31/64 drill.
Tapped 9/16-18?